
Honing Services: Precision Bore Geometry & Finish
Honing refines the inside diameter of a bore to extraordinary roundness, straightness, and surface finish using bonded abrasive stones. For hydraulic cylinders, bearing housings, and fuel systems where the bore must seal and run true, honing is the finishing step that makes it work. This guide covers how honing works, when to specify it, the materials it handles, and how to brief your shop.

How Honing Works
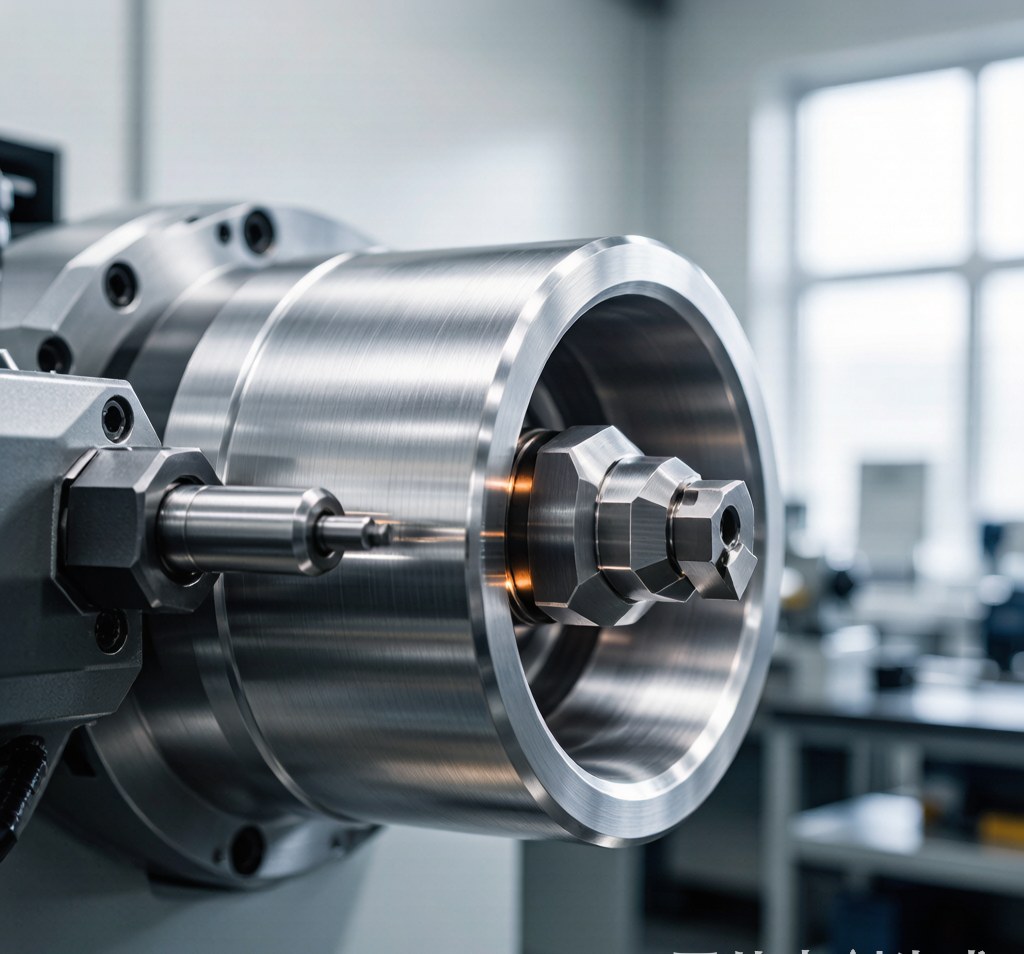
A honing head spins and reciprocates abrasive stones against the bore wall, removing a thin, controlled layer while generating a cross-hatch pattern ideal for oil retention. The process corrects geometry left by CNC boring or CNC milling, bringing the hole to final size and finish. It’s the standard follow-on when a bore must meet tight roundness and surface requirements.
Honing vs. Other Bore Finishes
Versus boring, honing achieves far finer finish and geometry. Versus cylindrical grinding (which can also finish IDs), honing is gentler and excels at long, thin bores. Choose honing when the bore needs a cross-hatch for lubrication and micron-level geometry.
Materials We Hone
- Cast iron and steel cylinders — hydraulic and engine blocks.
- Stainless and hardened alloys — for corrosive or wear service.
- Bronze and brass bushings — with tuned stone selection.
- Aluminum bores — with careful parameters.
- Carbide and ceramics — with diamond abrasives.
Industries That Rely on Honing
Hydraulics, automotive engines, aerospace actuators, and medical devices all need honed bores for sealing, lubrication, and load transfer. Bore geometry here directly affects leakage and life.
How to Spec Your Honing Job
- State final bore diameter and tolerance—honing holds microns.
- Define roundness, straightness, and taper limits.
- Specify surface finish (Ra/Rk) and cross-hatch angle.
- Note material and hardness for stone selection.
- Share bore depth and volume for tooling.
FAQ
What finish can honing achieve?
We regularly reach Ra 0.1–0.4 µm with controlled cross-hatch for oil retention.
Does honing correct a bad bore?
It corrects geometry within limits; severely out-of-round features should be pre-machined.
Can you hone hardened parts?
Yes. Hardened bores are a common honing application.
Why Choose Huaxiao for Honing
Our honing service delivers bore geometry and finish that seals and lasts, integrated with our machining and inspection. Send your drawing for a quote covering the full bore cycle.

