
Lapping Services: Sub-Micron Flatness and Mirror Finishes on Metal Parts
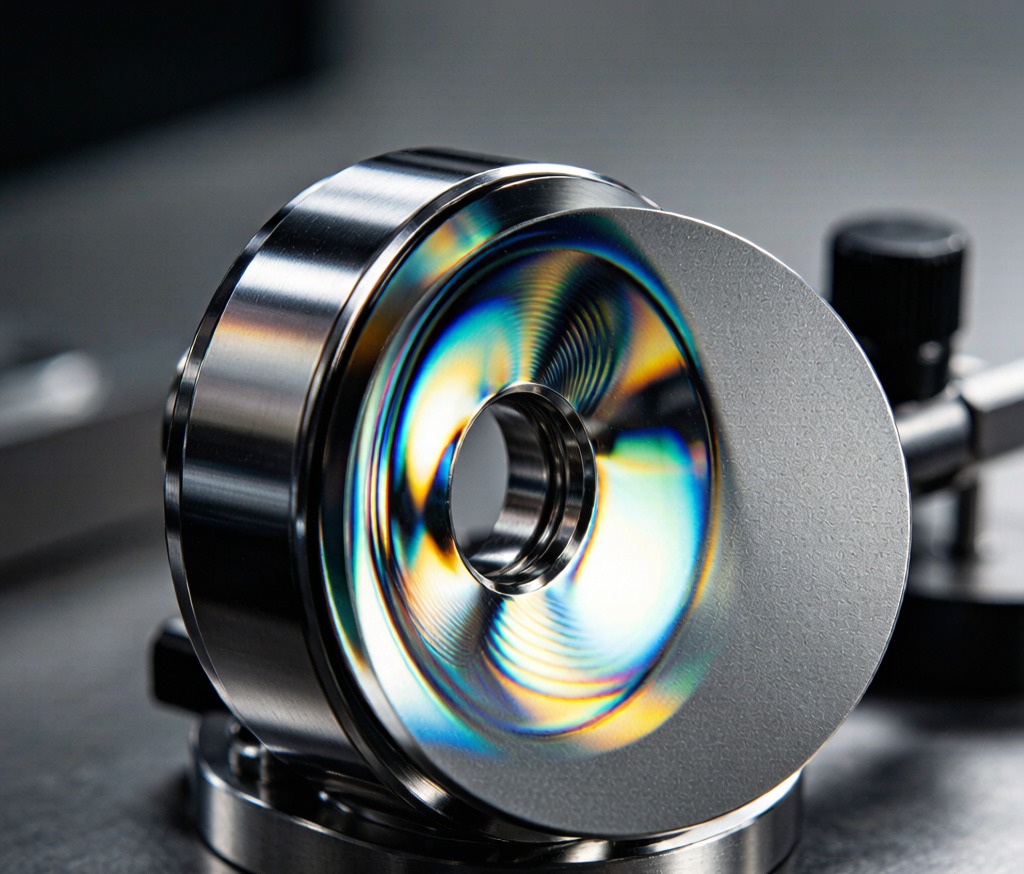
There is a point where grinding stops being enough. When a hydraulic valve plate must seal at 350 bar without an elastomer, when two mating faces must wring together, or when a print calls for 0.5 µm flatness across a 150 mm face, no grinder will get you there — the machine’s own spindle error […]

