
For high volumes and thin-wall accuracy, nothing beats stamped metal parts. Stamping forms, blanks, and pierces sheet in a single press stroke, driving unit cost down while keeping consistency near perfect. Huaxiao Parts builds progressive and compound tooling for brackets, terminals, shields, and clips produced in the millions, with the inspection discipline that high-rate lines demand. If your program is past the prototype stage and heading to scale, this article explains when stamping wins and how we manage it.
What Are Stamped Metal Parts?
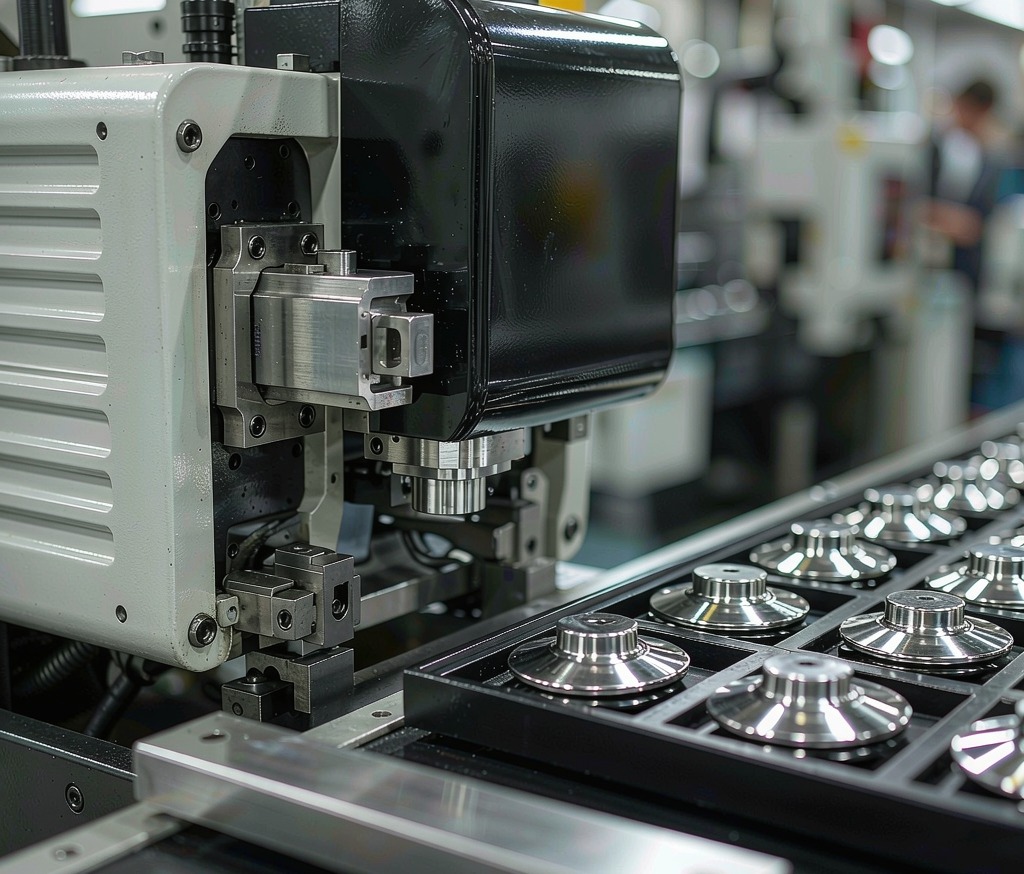
Stamping uses a press and hardened die to cut and shape sheet metal at high speed, producing a net-shape part that needs little or no secondary work. That is why it dominates high-volume hardware such as connectors, washers, spring clips, and mounting brackets where a tenth of a cent per piece decides margin. The die is the product: once it is qualified, every stroke repeats the same geometry within microns. The trade-off is upfront tooling cost, which is why stamping is a production solution rather than a prototype one. Good stamping houses design the die around your tolerances, not the other way around.
Progressive vs Compound Die Stamping
A progressive die stamping line carries the strip through stations that cut, form, and pierce in sequence, which is ideal for complex parts at speed because each hit adds a feature. Compound dies perform several operations in one stroke for simpler geometries and can be cheaper to build for lower feature counts. We select the route by volume and geometry, then simulate strip layout to minimize scrap between parts. The goal is the highest good-part rate at the lowest material waste, because offcut is the hidden cost in any stamping job.
Materials for Stamping
Low-carbon steel, stainless, spring steel, copper, and brass all stamp well, though each behaves differently under the punch. Material temper affects springback and how tightly it can bend without cracking, so we tune die clearance and plan to your specification rather than a generic setting. Coated and pre-finished stock can be stamped if the die protects the surface, which saves a finishing step later. We advise on grade so the part meets both form and function without premium alloy where standard steel would do.
Tolerances and Burr Control
We hold features to ±0.05 mm and control burr height under 10 percent of thickness, because a sharp edge can cut an operator or foul an assembly. After forming we deburr and can CNC punch secondary holes that the die cannot reach economically. For field service we apply powder coat or plasma cut trim, and the right corrosion protection keeps the part alive in its environment. Burr and edge quality are the details that separate a stamping house you trust from one that ships rejects.
When to Choose Stamping Over Machining
Above roughly five thousand pieces, stamping almost always wins on cost per part because the die cost is spread across the run. For lower volumes, precision stamping or laser-cut blanks may be cheaper because they avoid tooling entirely, even if the unit price is higher. The crossover point depends on part complexity and material, which is why we model both routes in the quote. Choosing wrong means paying for a die you never amortize or accepting a unit cost that kills margin.
Secondary Operations After Stamping
Most stamped parts need at least one follow-on step before they are usable, and planning those steps with the die saves money. We deburr and tumble to soften edges, then add secondary holes the die cannot reach economically, and apply finish or plate for corrosion resistance. For clip-style parts we can insert springs or rivets so the stamped piece ships as a working sub-assembly. Bundling these operations under one roof removes handoffs and the scrap and delay that travel between vendors causes, which is a quiet but real part of total cost.
If you are moving from prototype to production, send expected annual volume with the inquiry so we can propose the right die strategy from the start instead of re-tooling later. Early alignment on stamping route and material avoids a costly switch at scale, and sample parts from the actual production die confirm the process before you commit the run. The cheapest stamped part is the one designed correctly the first time, with tooling that amortizes across the volume you actually ship.
Frequently Asked Questions
How long does tooling take?
Prototype dies run in one to two weeks; production progressive dies take three to five weeks depending on complexity and validation needs.
Can you stamp very thin foil?
Yes, down to 0.1 mm with proper material handling, guide rails, and die clearance tuned for fragile strip.
Do you assemble stamped parts?
We rivet and weld stamped components into finished sub-assemblies on request, shipping a ready-to-install module.
What finishes work best on stamped steel?
Zinc or nickel plate resists corrosion on thin stampings, while powder coat adds color and abrasion resistance for visible parts; for stainless, passivation alone is often enough. We match the finish to whether the part sits inside a device or faces the weather, and we mask critical features so coating never blocks a hole or thread.
Ready to Start Your Project?
Get a build-ready quote on your custom metal parts within 24 hours. Share your drawing and our engineers will respond with process, lead time, and pricing.

