
Some defects hide where the eye cannot see: a crack running below a weld bead, porosity sealed inside a casting, a lack-of-fusion line buried in a joint. Cutting the part open to look would destroy it. Nondestructive testing (NDT) solves that problem, letting you verify internal and surface integrity without consuming the component. For buyers of welded, cast, or safety-critical machined parts, knowing which NDT method fits which defect is the difference between a verified shipment and a costly field failure.
The value of NDT is not only detection, it is confidence at scale. A method that finds one flaw in a sample part also gives you a documented basis to accept or reject a whole run, which is what lets production move without tearing parts apart. Used well, NDT turns an invisible risk into a managed, auditable condition.
Why NDT Matters for Metal Parts
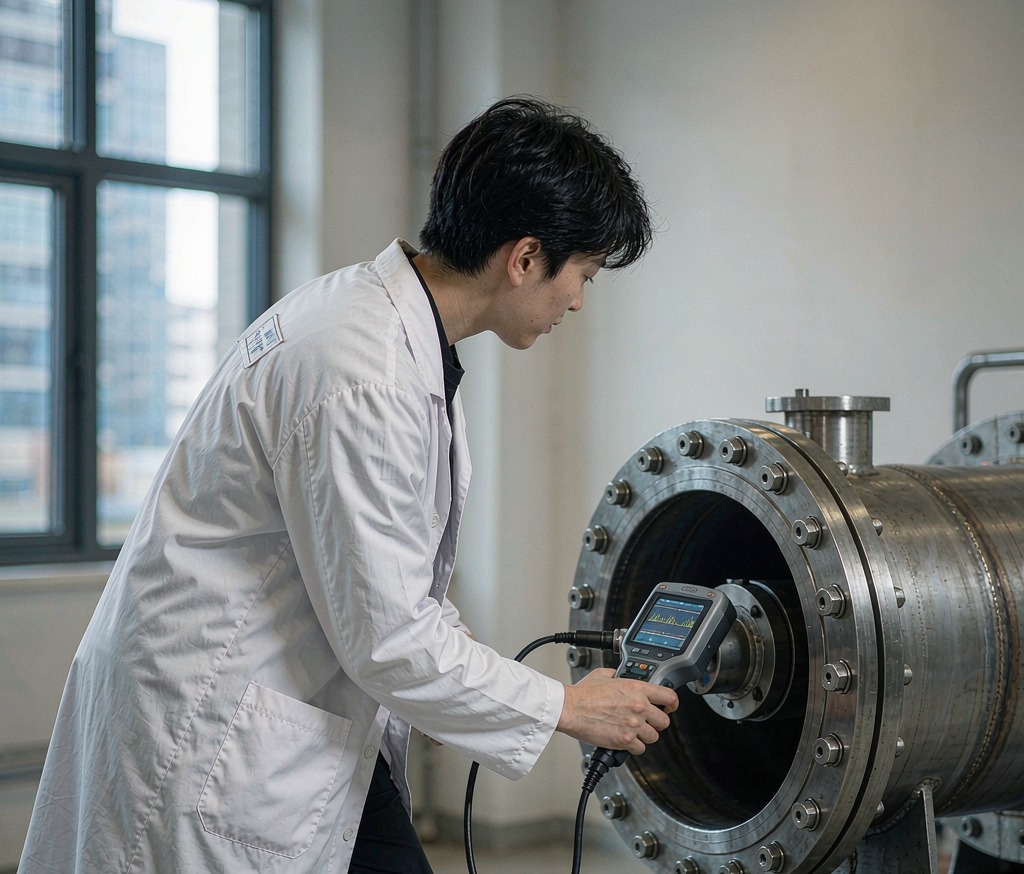
Machining can hold tight tolerances on the outside while a casting void sits undetected inside. Welds can look clean on the surface and still contain lack-of-fusion or cracks at the root. NDT gives you evidence about the parts you cannot see. Our welded assemblies and robotic welding work is frequently specified with NDT on critical joints, because a welded structure is only as strong as its weakest, invisible discontinuity.
Common NDT Methods Compared
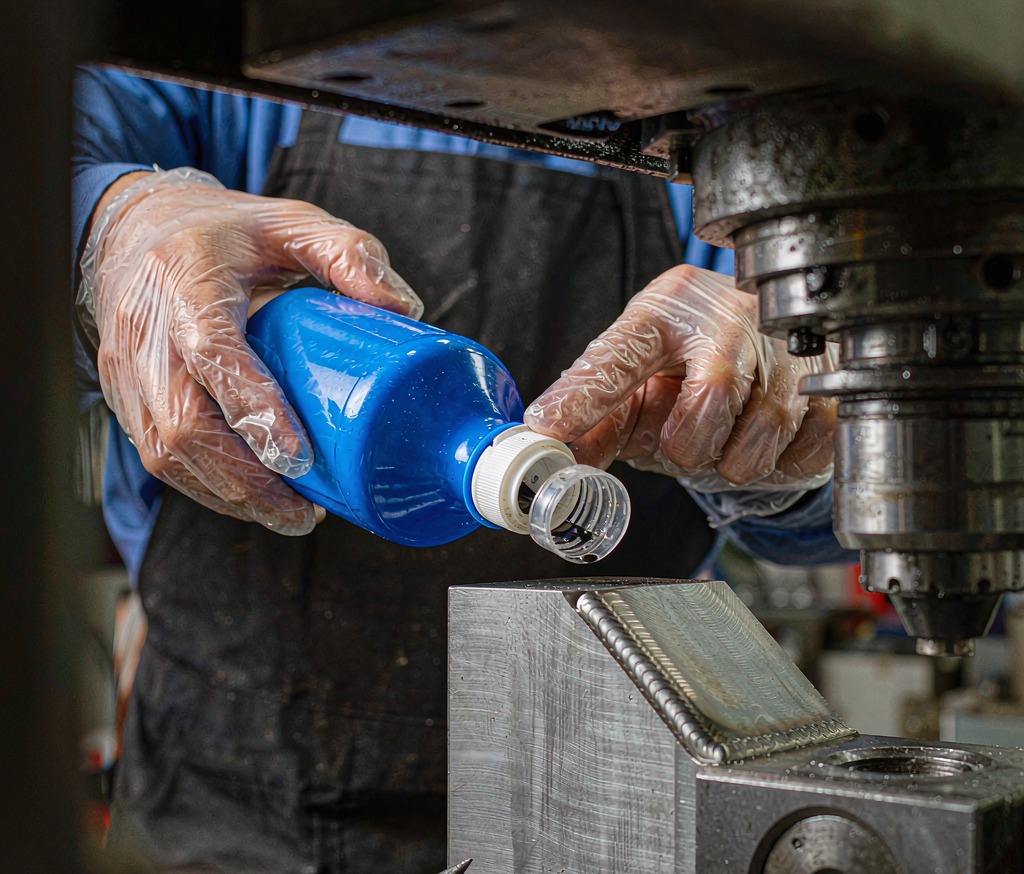
The four workhorses are liquid penetrant testing (PT), magnetic particle testing (MT), ultrasonic testing (UT), and radiographic testing (RT, or X-ray). PT finds surface-breaking defects on any material by drawing dye into the opening; it is cheap and simple but blind to subsurface flaws. MT uses a magnetic field to reveal surface and near-surface cracks in ferromagnetic steels. UT sends sound waves into the part and reads the echo, sizing internal flaws in thickness and position. RT produces an internal image, ideal for casting porosity and weld profiles. For a investment casting or a sand casting, X-ray is often the fastest way to confirm a sound section.
Two more methods deserve mention: eddy current testing for surface and near-surface flaws in conductive materials, and positive material identification for alloy verification. Neither replaces the big four, but both extend what a complete inspection plan can prove.
Choosing the Right Method by Defect Type
Match the method to the risk. Surface cracks in a ferromagnetic bracket call for MT. Hidden shrinkage in a cast housing calls for RT or UT. Thin welds on a die casting adjacent component are best checked with PT and UT depending on access. Heat-treated structural parts, where a missed flaw could be catastrophic, justify the higher cost of UT or RT. The method is a tool, not a status symbol, and the right choice depends on material, geometry, and the failure mode you are guarding against.
NDT for Castings, Welds, and Machined Parts
Castings need volumetric methods because their defects live inside. Welds need a combination: MT or PT for surface cracks, UT or RT for root and fusion defects. Machined parts usually need NDT only where a feature intersects a critical load path or where a prior process left risk. After heat treatment, a crack check confirms the part survived stress relief without developing a surface defect. The discipline is deciding, up front, which features are critical and which method proves them.
Standards and Acceptance Criteria
NDT is meaningless without an acceptance standard. Aerospace work follows NAS or customer-specific criteria, welds follow ASME or ISO codes, and castings follow graded reference radiographs. Specifying the standard on the drawing removes arguments at inspection time and gives the supplier a clear pass-fail line instead of a judgment call.
Cost vs Risk in NDT Selection
Budget pressure tempts teams to pick the cheapest method, but the right lens is cost of failure, not cost of test. A radiograph that catches a hidden shrink in a cast pump body prevents a far more expensive field replacement and a damaged customer relationship. The efficient move is risk-based: apply the heavier methods to the few features that actually carry load or seal pressure, and use simple PT or MT on the rest. That targeted approach keeps the inspection bill reasonable while still covering the defects that matter.
Building NDT Into Your Quality Plan
The strongest programs specify NDT at the drawing level: which features, which method, which acceptance standard. That removes ambiguity at inspection time and gives suppliers a clear target. Buyers can read more in our overview of metal part quality control and our notes on CMM inspection services, which cover the dimensional side that NDT complements. For welded structures specifically, our welded assemblies guide explains where joint inspection fits in the build sequence.
Frequently Asked Questions
Which NDT method is best for aluminum castings?
X-ray (RT) or ultrasonic testing are preferred for internal porosity and shrinkage, since aluminum is non-magnetic and MT does not apply. Penetrant testing handles surface defects.
Can NDT be done on finished, coated parts?
Often yes, but coatings can mask surface indications. PT and MT are usually performed before final coating, while UT and RT can sometimes read through thin coatings depending on the setup.
Is NDT required for every batch?
Not always. Many programs NDT the first article and then apply a sampling or process-capability plan, tightening inspection if the process drifts.
Specify NDT With Confidence
Choosing the right nondestructive test turns an unknown risk into a documented, accepted condition. Build it into the print and the quote, and your supply chain stops shipping surprises. The small added cost of NDT is almost always less than the cost of one field failure.
Ready to Start Your Project?
Get a build-ready quote on your custom metal parts within 24 hours. Share your drawing and our engineers will respond with process, lead time, and pricing.

