
When your part is small, complex, and needed in volume, two processes dominate: metal injection molding (MIM) and die casting. Both make net-shape metal parts at high rate, but they split on material, geometry, and tolerance. This comparison helps you pick the right one before you commit to tooling, because the wrong choice locks in cost you cannot recover across the program.
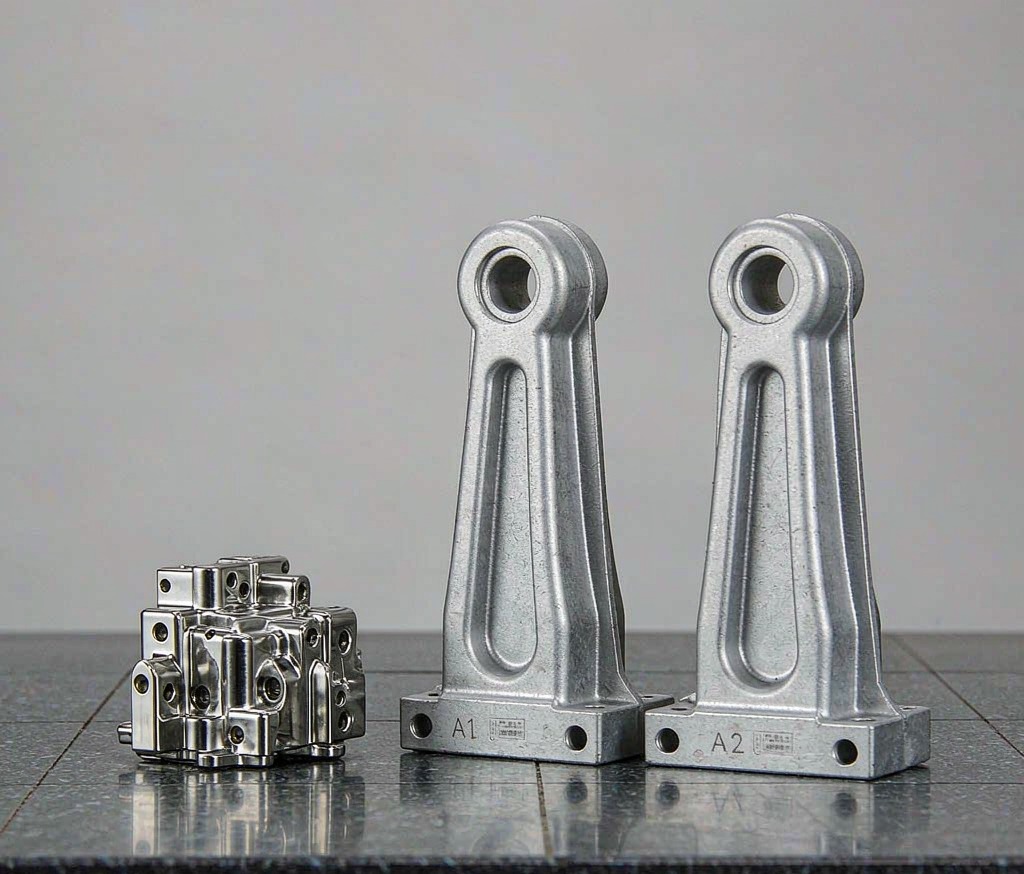
Two Ways to Make Small Complex Metal Parts
Die casting injects molten metal into a steel die at high pressure; MIM injects a binder-loaded metal powder through the same molding logic, then debinds and sinters. Both net-shape the part, but MIM reaches geometries die casting cannot fill. A metal injection molding service shines on parts with tiny features and tight tolerances that would need extensive machining if cast, while die casting owns larger, simpler shapes.
Volume and Tooling Economics
Die casting tooling is expensive but cycles in seconds, so it owns very high volumes of larger parts. MIM tooling is cheaper and cycles fast too, making it economical from lower break-even volumes on small parts. Your die casting service will quote tooling that only pays back in the hundreds of thousands; MIM often breaks even sooner because the mold is smaller and the sinter step needs no heavy press.
Materials Each Process Can Run
Die casting is built around zinc, aluminium, and magnesium. MIM runs stainless steels, low-alloy steels, tool steels, and even tungsten and titanium alloys die casting cannot handle. If your part needs 17-4 PH or 316L, MIM is usually the answer, often alongside investment casting for the larger siblings in the same family. Material alone often decides the process.
Geometry and Wall Thickness
MIM handles thinner walls and more intricate internal features, including undercuts that die casting would reject. Die casting needs draft and thicker sections for fill and ejection. Where the part is a small stainless bracket with ridges and holes, MIM forms it near-net; die casting would leave more to a CNC milling step. Think of MIM as the process for the part too detailed to cast cleanly.
Tolerances and Secondary Machining
MIM holds roughly plus or minus 0.3 percent of dimension as-sintered, better than die casting’s plus or minus 0.1 mm per 25 mm on small parts, and it needs little machining. Die casting may need more post-machining on tight features, finished by a surface grinding pass. Both can take a powder coating or anodizing finish for corrosion and appearance, so surface treatment is not the differentiator.
How to Choose for Your Program
Pick die casting for larger aluminium or zinc parts at extreme volume. Pick MIM for small, complex, high-alloy parts where machining would dominate cost. Our investment casting vs die casting guide covers the third option when the part is too big for MIM but too complex for die casting, and our powder metallurgy services note shows where PM overlaps MIM on small ferrous parts.
Common MIM vs Die Casting Mistakes
Buyers often pick the process by habit instead of by part. The costly mistake is sending a small, fine-feature stainless part to die casting, where it needs heavy machining, or pushing a large aluminium part to MIM, where the mold and sinter shrink fight you. Match the process to size, alloy, and volume first.
The other error is ignoring break-even volume. A MIM tool looks cheap next to a die cast die until you realize die casting pulls ahead at very high volume. Plot the crossover before you commit, and keep the design able to shift if volume changes after the first year.
MIM vs Die Casting Selection Checklist
Use these questions to steer the decision before you pay for a tool. They map directly to the cost and capability split between the two processes.
- If the part weighs under 100 grams and has fine features, lean toward a MIM injection molding route that forms the detail near-net.
- If the part is larger aluminium or zinc at extreme volume, a die casting tool will win on cycle cost per piece.
- If you need 316L or tool steel, die casting cannot run it, so investment casting or MIM are the realistic options.
- If tight tolerances sit on a sealing face, plan a light CNC milling finish regardless of which process forms the shape.
How do I know if my part is too big for MIM?
As a rule, MIM is economic below about 100 grams per part. Above that, the mold and sinter shrink make the part hard to control and casting becomes the better economic fit.
Frequently Asked Questions
Is MIM cheaper than die casting?
At low to mid volumes on small parts, usually yes, because MIM tooling is cheaper and needs less machining. At very high volumes of larger aluminium parts, die casting wins on cycle cost per piece.
Can MIM match die casting strength?
MIM runs higher-strength alloys like stainless and tool steel, so sintered MIM parts often outperform zinc or aluminium die castings in strength, though density is slightly lower than wrought stock. For small structural parts it is plenty.
Which has better surface finish?
Both are good as-molded. MIM gives a finer, more uniform surface on small features; die casting gives a smoother large-area finish. Either can be coated for appearance, so finish rarely drives the choice.
When would investment casting beat both?
When the part is too large for MIM and too complex or low-volume for die casting. Investment casting handles bigger, heavier, finer-detail parts that neither MIM nor die casting suits economically.
Ready to Start Your Project?
Get a build-ready quote on your custom metal parts within 24 hours. Share your drawing and our engineers will respond with process, lead time, and pricing.

