
TIG Welding Aluminum: Complete Settings & Technique Guide
Aluminum is one of the most weldable metals and one of the easiest to get wrong. Its soft oxide skin, high thermal conductivity, and low melting point punish sloppy setup with porosity, cracking, and weak beads. TIG welding services remain the preferred process when the joint must be clean, precise, and cosmetically flawless – exactly what aerospace, medical, and electronics buyers expect. This guide walks through the settings, filler choices, and technique that separate a sound aluminum TIG weld from a rejected one. If your part is already machined, see our aluminum CNC machining services for pre-weld prep.

Why Aluminum Needs a Different Approach
Three properties make aluminum unlike steel. First, the aluminum oxide layer that forms instantly on the surface melts at about 2,000°C while the base metal melts near 660°C – so the oxide must be removed or it traps inclusions. Second, aluminum conducts heat roughly three times faster than steel, pulling heat away from the arc and demanding higher amperage or tighter heat control. Third, it has no color change at the liquidus, so the welder must read the puddle by behavior, not by glow. Material choice matters too: pick the grade with our guide to choosing the right metal material.
Equipment and AC Settings
Aluminum is welded with alternating current (AC) TIG, not DC. The electrode-negative (EN) portion drives penetration; the electrode-positive (EP) portion blasts away the oxide. Modern inverters let you tune AC balance (typically 65-75% EN) and AC frequency (higher frequency tightens the arc for thin sections). The table below is a starting point for pure argon at ~15-20 CFH; refine on scrap.
| Thickness | Amperage | Tungsten | Filler | Argon (CFH) |
|---|---|---|---|---|
| 1 mm | 30-45 A | 1.6 mm ERW | 1.6 mm | 12-15 |
| 2 mm | 60-90 A | 2.4 mm | 2.4 mm | 15-18 |
| 3 mm | 100-130 A | 2.4 mm | 2.4 mm | 18-20 |
| 6 mm | 180-220 A | 3.2 mm | 3.2 mm | 20-25 |
Work with a shop that documents parameters per job – our TIG welding services include a welded sample report.
Aluminum Preparation Before Welding
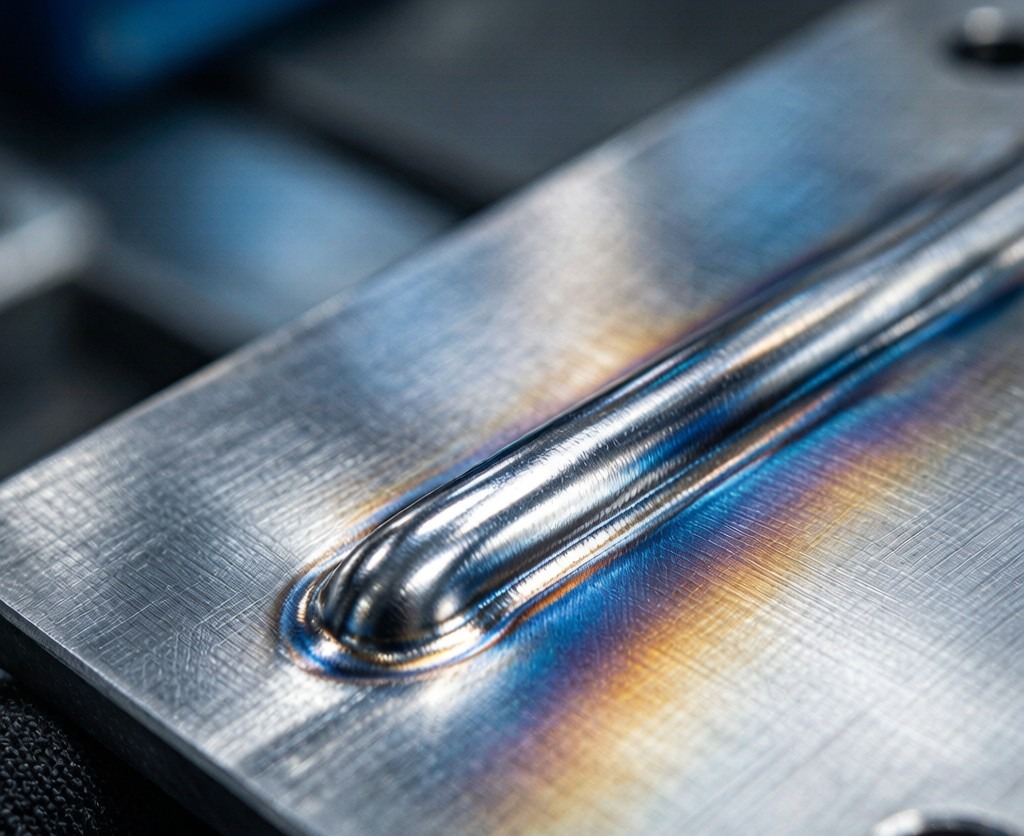
Cleanliness decides porosity. Degrease with a dedicated solvent (not shop rags soaked in oil), then remove the oxide with a stainless steel wire brush used only for aluminum, or a dedicated carbide burr. Brush in one direction and re-clean if the part sits more than a few hours. Final surface finish from metal surface treatment and proper passivation of nearby stainless parts keeps contamination out of the weld zone.
Filler Selection: ER4043 vs ER5356
Two fillers cover most work. ER4043 (~5% silicon) flows easily, produces a shinier bead, and resists hot-cracking on 6xxx alloys, but its lower strength and silicon sensitivity make it a poor choice near anodizing (it turns gray). ER5356 (~5% magnesium) is stronger and anodizes closer to the base color, favored for structural and marine work. For extrusions and frames, match the filler to the alloy with guidance from our aluminum extrusion team.
Technique: Stopping Porosity
Porosity is the #1 aluminum defect and almost always a cleanliness or shielding problem. Keep the torch angle steep, hold a tight cup-to-work distance, and never let the argon shield break. Pre-heat thick sections to ~150°C to slow heat loss, and use a slight push angle. When a weld must become part of a larger structure, our welded assemblies process adds fixturing and post-weld inspection.
Common Defects and Fixes
| Defect | Likely cause | Fix |
|---|---|---|
| Porosity | Moisture, oil, poor gas shield | Re-clean; check argon flow & leaks |
| Hot cracking | Wrong filler / high restraint | Use ER4043 or reduce joint stress |
| Tungsten contamination | Touching the puddle | Stop, regrind tungsten |
| Lack of fusion | Too fast / low heat | Raise amperage, slow travel |
TIG vs MIG for Aluminum
TIG wins on thin sheet, appearance, and short prototype runs; MIG welding services win on deposition rate for thicker parts and long production. For a full decision matrix, read our MIG vs TIG welding guide. Many production programs combine both – TIG for critical joints, MIG for fill.
When to Outsource to a Shop
If you need certified welds (AWS D1.2 for aluminum structures), repeatable quality, or welding combined with machining and finishing, outsourcing beats buying equipment. Our choosing a CNC supplier checklist and metal contract manufacturing model cover what to verify before you commit.
Frequently Asked Questions
Can you TIG weld cast aluminum?
Yes, but cast alloys (e.g., A356) are porous and silicon-rich, so pre-heat, slow travel, and ER4043 filler help. Hot-short cracking is a real risk, so qualify the procedure on a sample first.
Do I need AC or DC for aluminum TIG?
AC is required for aluminum because the EP half-cycle cleans the oxide while the EN half-cycle penetrates. DCEN will not weld aluminum cleanly.
Why does my aluminum weld turn black?
A dark, sooty bead means the oxide was not cleaned or the gas shield broke. A bright, silvery bead indicates a clean, well-shielded weld.
Ready to Start Your Project?
Get a build-ready quote on your custom metal parts within 24 hours. Share your drawing and our engineers will respond with process, lead time, and pricing.

